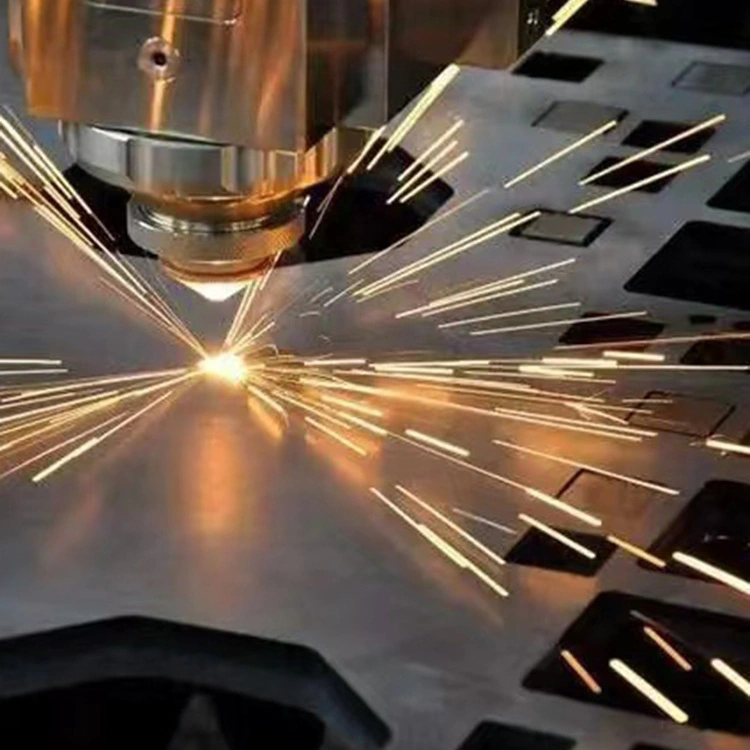
The landscape of modern manufacturing is shifting at an unprecedented pace, driven by the demand for more complex geometries, tighter tolerances, and exotic material compositions. For decades, laser cutting was largely confined to standard ferrous and non-ferrous metals, along with basic polymers. However, the evolution of resonator technology, beam delivery systems, and control software has shattered these limitations. Today, advanced laser cutting systems are not just tools; they are sophisticated fabrication centers capable of processing a range of materials that were once considered impossible or impractical to cut with light.
Understanding which new materials can now be processed with advanced laser cutting systems is critical for engineers, designers, and procurement specialists looking to innovate. Whether it is high-reflectivity copper alloys required for electric vehicle components or delicate composite materials used in aerospace, the capabilities of modern laser equipment have expanded dramatically. At Tianjin Shenghui Metal Products Co., Ltd., we have witnessed this evolution firsthand, integrating cutting-edge technology to ensure our factory remains at the forefront of this industrial revolution.
Content Directory
What Exotic Metals and Alloys Are Now Routinely Cut with Laser Cutting?
The term "exotic" in metallurgy typically refers to materials that are difficult to machine due to their hardness, toughness, or chemical reactivity. Traditional mechanical cutting methods often fall short when faced with these alloys, leading to high tool wear and slow throughput. However, with the latest advancements in laser cutting, we have broken down these barriers. Our factory routinely processes materials that would have destroyed tooling just a decade ago.
One of the most significant breakthroughs is in the processing of high-strength aerospace alloys such as Inconel, Hastelloy, and Titanium. These materials are essential for components that must withstand extreme temperatures and pressures. Advanced laser cutting systems utilize specific wavelength adjustments and pulse modulations to create a heat-affected zone so minimal that the material's structural integrity remains intact. We achieve this by using high-pressure assist gases that simultaneously cool the cut and expel molten material, preventing micro-cracking.
Another category that has seen massive growth is the processing of advanced high-strength steels (AHSS) used in the automotive industry. These steels, including press-hardened steel (PHS), are incredibly strong but notoriously difficult to trim. With our systems, we utilize multi-kilowatt fiber lasers that power through these materials with speed and precision that mechanical presses cannot match. The flexibility of our laser cutting setups allows for rapid prototyping and low-volume production runs without the need for expensive hard tooling.
Furthermore, the ability to cut high-purity metals used in the medical and electronics industries has improved. Tantalum, used for surgical implants, and Molybdenum, used for semiconductor components, are now processed daily in our factory. The precision of our equipment ensures that there is no contamination, which is vital for biocompatibility and electronic performance. Below is a table detailing the specifications of our primary laser cutting systems used for these advanced metals.
|
Material Category
|
Specific Alloys
|
Laser Type
|
Max Thickness (mm)
|
Assist Gas
|
|
Superalloys
|
Inconel 718, Hastelloy C-276
|
Fiber Laser (6kW - 12kW)
|
20 mm
|
Nitrogen / Argon
|
|
High-Strength Steels
|
Usibor 1500, Ductibor 500
|
Fiber Laser (8kW - 15kW)
|
30 mm
|
Compressed Air / Nitrogen
|
|
Refractory Metals
|
Molybdenum, Tantalum, Tungsten
|
Green Wavelength Fiber Laser
|
8 mm
|
Argon
|
|
Titanium Alloys
|
Grade 5 (Ti6Al4V), Grade 23
|
Fiber Laser (4kW - 8kW)
|
25 mm
|
Argon (to avoid oxidation)
|
This table demonstrates the technical capability we possess at Tianjin Shenghui Metal Products Co., Ltd. Our investment in diverse laser sources allows us to tailor the cutting process to the specific metallurgical properties of the workpiece. We do not rely on a one-size-fits-all approach; instead, we match the laser's wavelength and power to the material's absorption characteristics. This ensures that when you ask "Which new materials can now be processed with advanced laser cutting systems?" the answer is almost always a resounding "Yes" when you partner with us.
How Do Advanced Systems Handle Reflective and Composite Materials?
Historically, reflective materials like copper, brass, and aluminum were the bane of laser cutting. The laser beam would bounce back into the resonator, causing catastrophic damage to the optics and the laser source itself. Similarly, composite materials, with their heterogeneous structure, presented challenges due to differing vaporization points of the matrix and the reinforcement. So, how have advanced laser cutting systems overcome these hurdles?
The solution for reflective materials lies in the adoption of advanced fiber laser technology with built-in back-reflection protection. Unlike older CO2 lasers, modern fiber lasers utilize a solid-state gain medium. Our systems are equipped with sensors that detect back reflections instantly. If a spike in reflected energy is detected, the system adjusts the pulse parameters or momentarily shuts down the beam to protect the cavity. Furthermore, the shorter wavelength of fiber lasers (typically 1.07 micrometers) is absorbed more readily by copper and brass than the longer wavelength of CO2 lasers. This means that instead of reflecting, the energy is efficiently converted into heat, allowing for clean, fast cuts.
Regarding composites, the processing of materials such as Carbon Fiber Reinforced Polymers (CFRP) and Glass Fiber Reinforced Polymers (GFRP) has become a reality. The key here is not just power, but pulse duration. We utilize ultra-short pulse lasers (picosecond or femtosecond) that vaporize material through sublimation rather than melting. This "cold ablation" process ensures that the carbon fibers are cut cleanly without melting the surrounding polymer matrix, which would lead to a rough edge and delamination.
Our factory has also perfected the cutting of multi-layer materials used in modern electronics and insulation. These often consist of a polymer film bonded to a metallic foil. Traditional cutting would smear the layers together. With our advanced beam shaping optics, we can adjust the focal point to cut precisely through the stack without distorting the individual layers. Here are the key capabilities we offer for these difficult materials:
-
Reflective Metals: Pure Copper (up to 6mm), Brass (up to 8mm), and High-Silicon Aluminum.
-
Thermal Composites: Carbon Fiber Prepreg and Cured CFRP (up to 10mm) with minimal charring.
-
Laminates: Copper-Clad Laminates (CCL) for PCB manufacturing, cut with zero burr.
-
Coated Materials: Galvanized steel and Aluzinc, cut with edge sealing to prevent corrosion.
At Tianjin Shenghui Metal Products Co., Ltd., we have dedicated workstations specifically configured for these materials. Our engineers understand the nuances of beam interaction with dissimilar materials. We do not simply process these items; we analyze the material composition to determine the optimal feed rate and gas combination. This technical expertise is the foundation of our reputation and why clients trust us with their most challenging projects. When they need to know which new materials can now be processed with advanced laser cutting systems, they look to our track record of success.
Why Are Non-Metal Materials Like Ceramics and Sapphire Now Viable?
The transition of laser cutting from a purely metalworking tool to a universal processing solution is best exemplified by its application on hard, brittle non-metals. Materials such as technical ceramics (alumina, zirconia), sapphire, and specialized glass are notoriously difficult to shape. They are prone to cracking under thermal stress and are harder than most cutting tools. However, the question of which new materials can now be processed with advanced laser cutting systems includes these very substances, thanks to innovations in laser wavelength and beam control.
Traditional lasers struggled with ceramics because they are transparent or reflective to infrared light. Our approach utilizes either CO2 lasers (with a longer wavelength that is absorbed by the ceramic lattice) or, more recently, green and UV lasers. For instance, when cutting sapphire, which is used for high-durability watch faces and smartphone camera covers, we employ a technique called "filamentation." An ultra-short pulse laser is focused inside the material. The high intensity creates a plasma filament that modifies the material internally, creating a separation line with virtually no surface damage. The parts are then separated with a gentle mechanical force, yielding pristine edges.
For conductive ceramics like Silicon Carbide (SiC), used in power electronics, we utilize a multi-step process. First, a low-power beam scores the material. Then, a controlled breaking process separates the parts. This ensures that the delicate electrical properties of the SiC are not compromised by micro-cracks. Our laser cutting systems are equipped with precision stages that move the material under a stationary beam, ensuring absolute accuracy and minimizing vibration that could shatter the workpiece.
The viability of processing these materials opens up new design possibilities across industries. In medical technology, zirconia dental implants and surgical tools can now be cut to custom geometries in minutes rather than days. In the semiconductor industry, the ability to cut glass interposers and ceramic substrates precisely is enabling the next generation of miniaturized electronics. Below is a list of the non-metal materials our factory currently processes, showcasing the breadth of our capabilities:
-
Technical Ceramics: Alumina (Al2O3), Zirconia (ZrO2), Silicon Nitride (Si3N4).
-
Crystalline Materials: Synthetic Sapphire, Quartz, and Ruby.
-
Specialty Glass: Borosilicate, Gorilla Glass, and Fused Silica.
-
Natural Materials: High-density Graphite and Carbon-Carbon composites.
This expansion into non-metals represents a significant investment in expertise at Tianjin Shenghui Metal Products Co., Ltd. We have trained our technicians specifically in the art of brittle material processing. It requires a different mindset than cutting steel; patience and precision are paramount. By mastering these techniques, we provide our clients with a single source for all their precision fabrication needs, whether they are working with inch-thick steel or wafer-thin sapphire. The question of which new materials can now be processed with advanced laser cutting systems is answered daily on our factory floor.
Summary: The Future of Material Processing
The journey of laser cutting technology is one of constant expansion. From its early days as a niche tool for cutting thin sheets, it has evolved into a versatile, indispensable process for modern industry. We have explored how reflective metals, superalloys, composites, and even brittle ceramics are now within the realm of possibility. This evolution is driven by the synergy of advanced laser sources, intelligent control systems, and deep metallurgical and material science knowledge.
For businesses looking to stay competitive, understanding which new materials can now be processed with advanced laser cutting systems is not just an academic exercise; it is a strategic advantage. It allows for the consolidation of supply chains, the reduction of lead times, and the creation of products with performance characteristics previously unattainable. At our factory, we are committed to pushing these boundaries further. We continuously test new materials and refine our processes to ensure that when our clients have a challenging project, we are ready to deliver.
If you are looking to leverage the latest advancements in laser cutting for your next project, we invite you to contact us. Let Tianjin Shenghui Metal Products Co., Ltd. be your partner in innovation. Our team is ready to provide you with a detailed analysis and quotation for your specific material processing needs. Experience the precision and capability of our advanced Laser Cutting systems today.
Frequently Asked Questions (FAQ)
Which new materials can now be processed with advanced laser cutting systems that were impossible a decade ago?
A decade ago, highly reflective materials like pure copper and brass were extremely difficult to process due to the risk of back-reflection damaging the laser source. Today, advanced fiber laser systems, like those used at Tianjin Shenghui Metal Products Co., Ltd., are equipped with back-reflection protection and shorter wavelengths that are readily absorbed by these metals. Additionally, brittle non-metals such as technical ceramics (alumina, zirconia) and crystalline materials like sapphire are now routinely cut using ultra-short pulse lasers that perform "cold ablation," preventing thermal cracking. These advancements have effectively doubled the range of processable materials, allowing for innovation in electronics, aerospace, and medical device manufacturing.
How does laser cutting quality compare for new materials like CFRP versus traditional metals?
The quality metrics differ because the failure modes are different. For traditional metals, quality is measured by edge roughness (Ra) and dross. For new materials like Carbon Fiber Reinforced Polymer (CFRP), the primary concern is the Heat Affected Zone (HAZ) and delamination. Advanced laser cutting systems address this by using pulsed fiber lasers or UV lasers that minimize heat input. At our factory, we achieve what is called a "dry cut" on CFRP, where the matrix material does not melt or burn, and the fibers are sheared cleanly. This results in a cut quality that is often superior to mechanical milling because there is no tool wear or vibration, ensuring consistent edge quality across thousands of parts, which is vital for aerospace structural components.
What are the limitations when processing high-reflectivity metals with modern laser cutting systems?
While modern systems have overcome the primary risk of back-reflection, there are still practical limitations. The main limitation is thickness. While we can cut copper up to 6mm reliably, cutting thicker sections (above 10mm) becomes challenging due to the material's high thermal conductivity, which dissipates heat away from the cut zone quickly. This can lead to a slower cutting speed compared to steel of the same thickness. Additionally, the purity of the material matters; oxygen-free high conductivity (OFHC) copper cuts differently than electrolytic tough pitch (ETP) copper. Our engineers at Tianjin Shenghui Metal Products Co., Ltd. account for these nuances by adjusting the focal position and using nitrogen at very high pressures to ensure a clean, burr-free edge, but understanding the specific alloy chemistry is key to a successful outcome.
Can advanced laser cutting systems process coated or painted materials without damaging the coating?
Yes, this is one of the significant advantages of modern laser cutting. When processing pre-painted or coated metals, the goal is often to cut through the metal without chipping the coating on the surface or burning it back from the cut edge. This is achieved through what is known as "coating-friendly cutting." By using a fiber laser with a very small kerf width and optimizing the pulse shape, we can vaporize the metal while leaving the surrounding coating intact. For materials like Galvanized steel, we also utilize specialized cutting parameters that minimize zinc vaporization at the cut edge, which reduces the formation of zinc oxide (white rust) post-process. Our laser cutting systems are programmed with specific recipes for these materials to ensure the aesthetic and protective qualities of the coating are preserved.
What specific laser parameters are most critical for cutting new technical ceramics and glass?
For technical ceramics and glass, the most critical parameter is no longer just power, but wavelength and pulse duration. These materials are transparent to standard infrared fiber lasers, so they require either a CO2 laser (9.3µm to 10.6µm wavelength) which is absorbed by the silica structure, or a green/UV laser for high-precision "cold cutting." Pulse duration is equally important; we use picosecond or femtosecond pulses. This is incredibly short (one quadrillionth of a second), which delivers energy so fast that the material sublimates directly from solid to gas without melting. This "cold ablation" process is essential to prevent micro-cracking and heat stress in the ceramic matrix. Additionally, the focal point positioning must be controlled with sub-micron accuracy to ensure the cut is vertical and precise.
 English
 Español
 Português
 русский
 Français
 日本語
 Deutsch
 tiếng Việt
 Italiano
 Nederlands
 ภาษาไทย
 Polski
 한국어
 Svenska
 magyar
 Malay
 বাংলা ভাষার
 Dansk
 Suomi
 हिन्दी
 Pilipino
 Türkçe
 Gaeilge
 العربية
 Indonesia
 Norsk
 تمل
 český
 ελληνικά
 український
 Javanese
 فارسی
 தமிழ்
 తెలుగు
 नेपाली
 Burmese
 български
 ລາວ
 Latine
 Қазақша
 Euskal
 Azərbaycan
 Slovenský jazyk
 Македонски
 Lietuvos
 Eesti Keel
 Română
 Slovenski
 मराठी
 Srpski језик